
Faster pallet movement depends on more than replacing a driver with sensors: the stacker, rack, floor, pallets, software, traffic controls, and recovery process must work as one system. By the end, you will be able to define the automation architecture, test whether your site is suitable, compare alternatives, and judge performance claims before requesting quotations.
Key takeaways
- Confirm aisle width, floor quality, rack layout, and pallet consistency first.
- Size capacity, lift height, travel distance, and duty cycle together.
- Test obstacle detection, emergency stops, recovery states, and handover points.
- Choose manual or assisted handling when exceptions and layout changes dominate work.
What a fully automatic stacker actually does
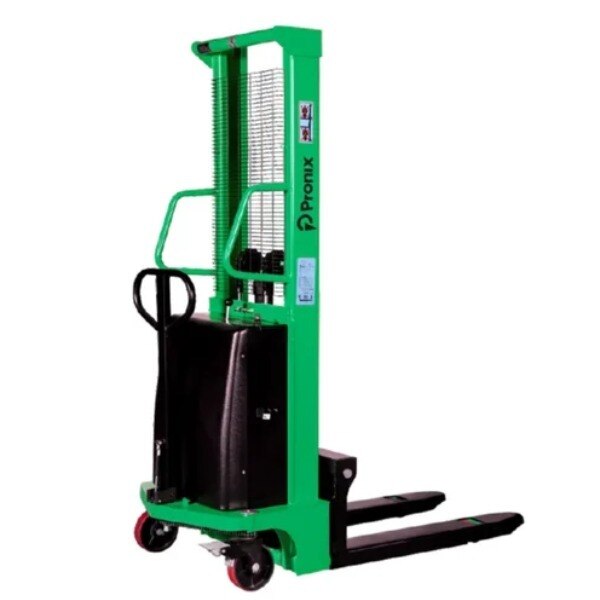
“Fully automatic” means the truck executes a warehouse mission without a driver steering, lifting, or confirming each movement. A control system assigns the task, while navigation, scanners, load sensors, obstacle detection, and safety controls manage movement; an exception sends the pallet or vehicle to a defined recovery state.
The term fully automatic stacker can describe two different architectures:
| Architecture | How the pallet moves |
|---|---|
| Automated guided industrial truck | Travels between pickup and storage locations using mapped routes, markers, or navigation software. |
| Stacker crane | Runs on fixed rails inside an automated storage-and-retrieval system and serves dedicated rack positions. |
Confirm the architecture before comparing quotations. Their aisle, guarding, floor, rack, and software requirements differ.
A complete mission normally follows this sequence:
- The system receives a pallet location and destination from the warehouse-control system.
- The vehicle reaches the pickup point, verifies the pallet ID and position, and performs pallet pickup and placement onto its forks or load platform.
- It travels to the destination while controlling speed around people, vehicles, and obstructions.
- It aligns with the rack or floor position, lifts to the commanded height, and deposits the pallet.
- Sensors confirm that the load is stable and fully clear, then the vehicle returns to a designated lane, charging point, or next assignment.
A failed scan, skewed pallet, blocked aisle, low battery, or lost navigation reference must trigger a documented recovery procedure, not an improvised manual entry into the aisle.
The site conditions that determine whether automation works
Control the rack, aisle, floor, pallet, traffic routes, and recovery arrangements before installation. A narrow-aisle automated guided industrial truck needs a clear travel path, while a fixed stacker crane needs a guarded storage aisle built to its rail and mast geometry.
| Architecture | Conditions to verify | Failure if wrong |
|---|---|---|
| Automated guided industrial truck | Marked routes, pedestrian separation, navigation references, charging or battery-swap space | Obstacle stops, route loss, and unsafe aisle entry |
| Fixed stacker crane | Rail alignment, rack anchoring, guarding, fire access, and accurate storage locations | Structural interference, inaccessible stock, or a prolonged shutdown |
Check these site conditions against measured drawings and actual pallets:
- Confirm the rack type, beam clearances, load ratings, column protection, and the required placement tolerance. A pallet that fits the bay width can still strike a beam or overload the rack.
- Measure aisle width at its narrowest point, including protruding loads, fire equipment, doors, and pedestrian crossings.
- Survey floor flatness, level, joints, cracks, load capacity, and slope. Uneven concrete can reduce navigation accuracy, increase wheel wear, and cause a raised load to sway.
- Verify pallet compatibility: overall dimensions, fork length and spread, fork-section clearance, entry direction, bottom-board arrangement, single- or double-face construction, and damaged-pallet limits.
- Define traffic separation, emergency-stop access, lighting, network coverage, and charging ventilation before commissioning. Apply ISO 3691-4 to driverless industrial trucks, then check local machinery and workplace-safety law separately.
- Require mission tests using the real pallet mass and lift height. Record travel distance, battery state of charge, congestion, acceleration limits, scanning, waiting, pickup and deposit accuracy, and exception recovery—not just an empty-truck cycle claim.
How to size the stacker and compare equipment options
Start with the capacity chart, not the headline kilogram rating. Require rated capacity and residual capacity at your actual load centre, lift height, attachment, and pallet condition; capacity falls as the mast rises. A 1,500 kg label does not prove safe placement on a high rack.
| Architecture | Compare | Evidence required |
|---|---|---|
| Guided automatic truck | Aisle width, turning radius, crossings, and traffic direction | Route map showing loaded-truck clearances and stopping points |
| Fixed stacker crane | Rack bay depth, storage height, and load-transfer positions | ASRS layout with rack, shuttle, and conveyor interfaces |
| Semi-automatic stacker | Operator handoff and automated travel limits | Defined mission boundary and control responsibility |
Match the machine to the actual load carrier. Confirm fork length, fork spread, fork-section dimensions, entry direction, bottom-board arrangement, and single- or double-face pallet design; nominal pallet length and width are not enough.
Ask for these figures in the purchase specification:
- Maximum pallet mass and dimensions, including damaged-pallet limits and overhang tolerance.
- Capacity chart at every required lift height and load centre, with the installed fork or attachment.
- Rack beam clearances, minimum aisle width, maximum floor slope, joint height, flatness, and loaded floor capacity.
- Travel and lift speeds with a full load, plus acceleration limits, pickup and deposit accuracy, and stopping distance.
- Mission assumptions covering one-way routes, intersections, pedestrian exclusion zones, charging pauses, and simultaneous vehicle traffic.
Compare complete mission time, not an empty-truck cycle claim. The test must include travel distance, pallet mass, lift height, scanning, waiting, and exception handling.
How to measure speed, safety, utilities, and system integration
A supplier must define a complete warehouse mission, not advertise an isolated cycle time. The baseline must state the architecture: an automated guided industrial truck or a fixed stacker crane in an automated storage-and-retrieval system, because each needs different aisle, guarding, floor, fire-safety, and integration provisions.
1. Measure cycle time from dispatch to confirmed deposit, then return to the designated lane. Record travel distance, lift height, pallet mass, battery state of charge, aisle congestion, acceleration limits, pickup and deposit accuracy, scanning, waiting, and exception handling.
Ask for cycles per hour at your real load and traffic conditions, plus mean time to recover and the percentage of faults needing manual aisle entry.
2. Require a safety design against ISO 3691-4 covering operating modes, speed control, navigation, emergency stops, obstacle detection, and pedestrian interaction. Define safe-stop, restart, and manual-rescue procedures; compliance with ISO 3691-4 does not replace local machinery or workplace-safety law.
3. Specify utilities with operating loads and limits: electrical supply, battery charging or battery-swap capacity, charging locations, network coverage, and any compressed-air demand. Survey leaks ultrasonically, use engineered blow-off nozzles, and isolate idle zones instead of raising compressor pressure, which increases leakage and actuator wear.
4. Write the warehouse management system or warehouse-control interface before purchase. Define pallet identity, destination confirmation, occupied-location status, fault codes, network-loss behavior, audit records, and restart permissions.
The recovery plan must cover missing or skewed pallets, blocked aisles, failed scans, low battery, lost navigation reference, and communication timeouts. Without those definitions, a fast nominal cycle can still create inventory errors and unsafe restarts.
When a fully automatic stacker is the wrong choice
Irregular pallets, mixed load centres, and frequent manual exceptions can make automation slower and less safe than a competent operator. Delay the project if you cannot enforce pallet dimensions, floor condition, rack locations, pedestrian separation, and a recovery process for blocked aisles or failed scans.
| Condition | Better decision | Why |
|---|---|---|
| Unstable pallet quality or changing load sizes | Electric forklift or electric reach stacker | An operator can judge a leaning load, adjust fork entry, and handle changing rack positions. |
| Short moves between staging and production | Electric pallet truck | A full navigation system adds integration and recovery work that the distance does not justify. |
| Occasional loads with low volume | Hand pallet truck | The purchase, mapping, charging, and maintenance burden can exceed the labour saved. |
| Narrow, uneven, or frequently obstructed aisles | Redesign the site first | Navigation references, braking distance, rack clearance, and pedestrian controls need predictable space. |
| High exception rates or no recovery team | Delay automation | A missing pallet, communication timeout, or low battery becomes downtime rather than a quick correction. |
| Fire, guarding, or aisle changes still under design | Delay and define the architecture | An automated guided truck and a fixed stacker crane require different guarding, floor, fire-safety, and integration plans. |
For any automated guided truck, require evidence against ISO 3691-4 and local workplace law, plus mean time to recover and the percentage of faults requiring aisle entry. If pneumatic gates or stops support the system, SS Quality Air Solutions can help document pressure, air consumption, filtration, and fail-safe behaviour before approval.
Frequently asked questions
What does a fully automatic stacker do?
It completes assigned warehouse missions without a driver steering, lifting, or confirming every movement. Navigation, scanners, load sensors, obstacle detection, and safety controls manage the task, while exceptions trigger a defined recovery state.
Which site conditions affect automatic stacker performance?
Check aisle width, floor flatness, rack geometry, lighting, traffic separation, pallet dimensions, load stability, pedestrian access, and the reliability of location markers or navigation references.
How do you size and compare fully automatic stackers?
Compare rated load capacity, lift height, mast configuration, aisle turning space, travel distance, battery runtime, charging method, cycle time, pallet dimensions, and duty cycle against your real warehouse missions.
When is a fully automatic stacker the wrong choice?
Automation is a poor fit when pallets vary heavily, aisles change frequently, loads are unstable, exceptions require constant human judgment, or the expected volume cannot justify integration and maintenance effort.